Custom Rotary Valve Design: Essential Tips for Bulk Material Handling
2026-10-31
Bulk material handling rarely gets the attention it deserves—until a poorly sized valve causes bridging, leakage, or a costly shutdown. Custom rotary valves are often the difference between a process that hums and one that constantly fights you. At AVM, we've seen how the right design choices—rotor clearance, material properties, pressure differentials—can transform throughput and reliability. This guide unpacks the essential tips you need before specifying your next custom rotary valve, so you can avoid the common pitfalls and keep your material flowing exactly as intended.
Map Your Material's Flow Traits Before Welding Anything
Most welders jump straight to the torch without ever watching how the base metal behaves under heat. That's a costly habit. Aluminum flows like water once it hits temperature, while stainless steel stays sluggish and demands a tighter arc. If you don't know which one you're dealing with, you'll fight the puddle all day—or worse, blow through the joint. Take ten minutes on a scrap piece and run a bead with your usual settings. Watch the puddle spread, the wetting angle at the toes, and how fast it freezes. That single test tells you more than any spec sheet.
Mapping flow traits isn't about memorizing charts—it's about building a mental picture of how the metal moves when you add filler. On a clean piece of 6061, you'll see the puddle push outward evenly and accept rod without hesitation. Try the same on cast aluminum and the surface will look grainy, with the bead sitting high because the oxides won't let it wet out. Write these observations down with the exact amperage, travel speed, and gas flow. After a few jobs, you'll have a personal reference that beats anything a textbook gives you.
Ignoring this step leads to classic failures: cold lap on thick steel because you didn't realize it was heat-sinking faster than your travel speed, or undercut on titanium because the molten pool ran ahead of the arc. High-alloy steels can suddenly become fluid at a narrow temperature window, catching you off guard mid-pass. Before you light up on production work, do a quick flow check—adjust your pulse frequency, switch to a larger cup, or back off the amps based on what the material shows you. It's five minutes that saves a rework.
Abrasion Patterns That Reveal the Right Rotor Coating
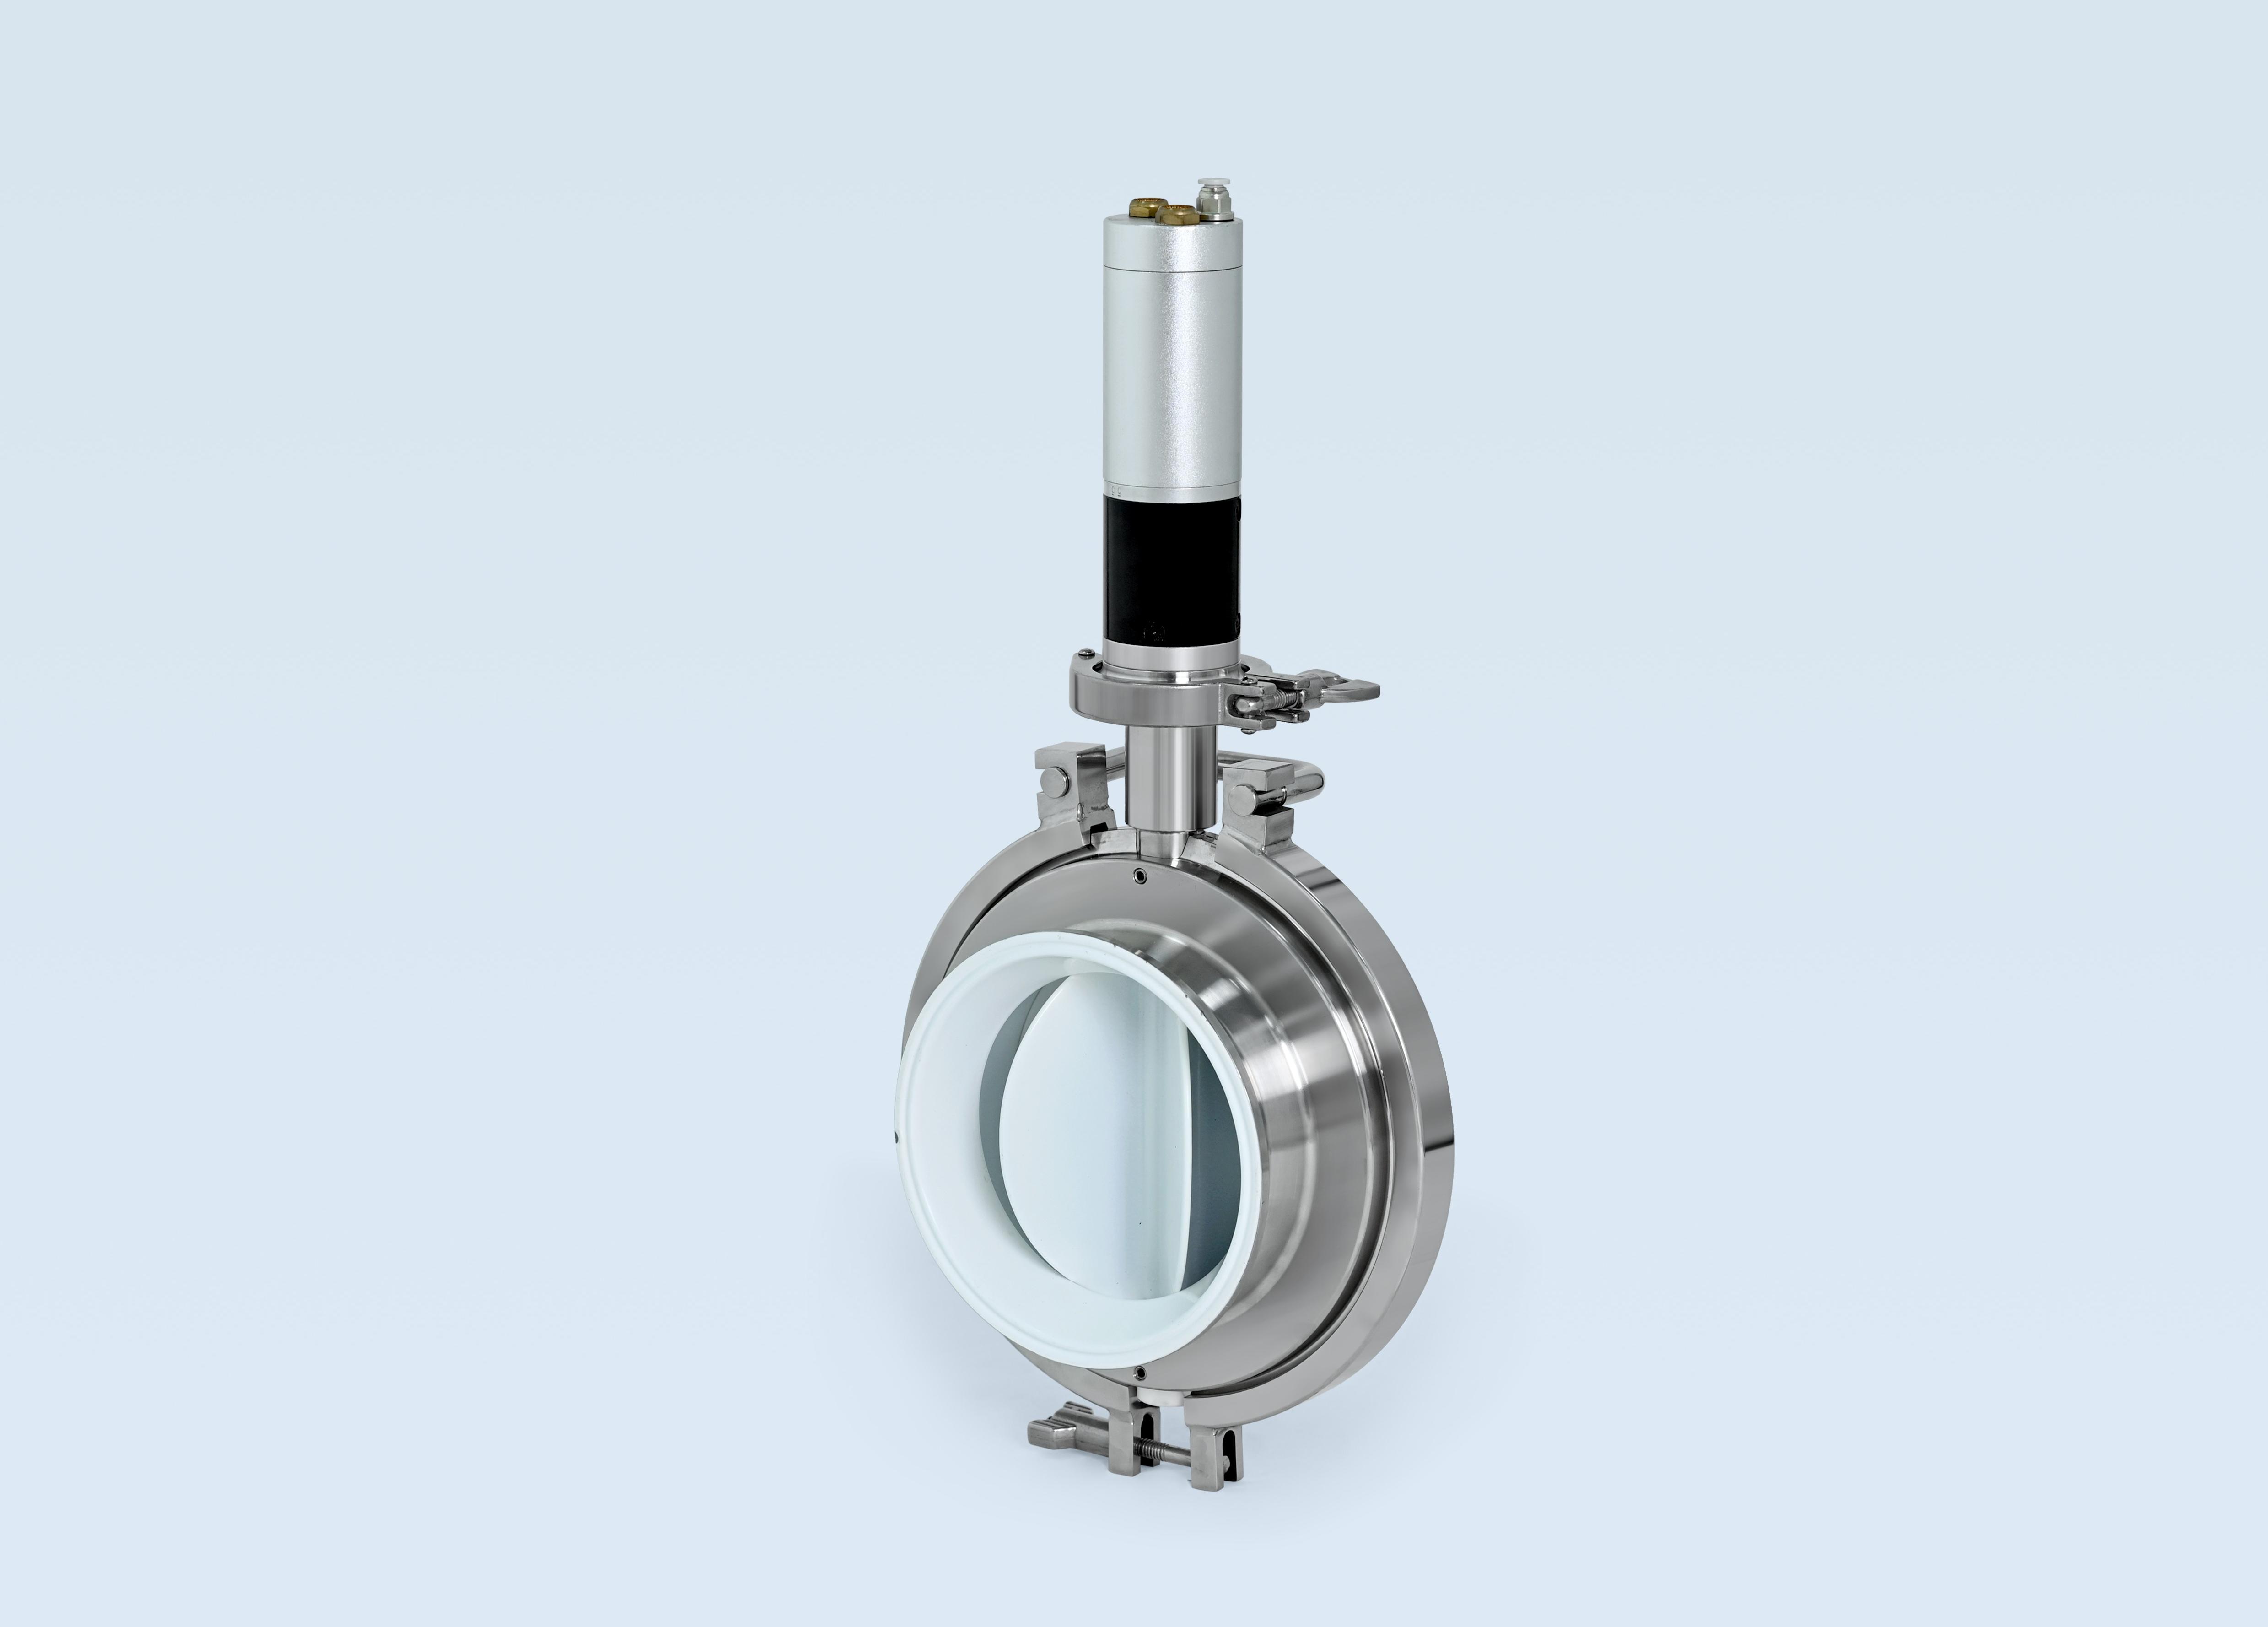
When you look closely at a rotor that has seen some real-world use, the wear marks tell a story that a fresh-out-of-the-box inspection never will. A coating that is doing its job tends to fail in predictable ways: fine, uniform scuffing across the friction face suggests an even distribution of thermal load and no localized hot spots, whereas patchy, deep scoring at the outer edge often points to a mismatch between the pad compound and the coating's hardness. The subtle difference between a surface that has simply polished over time and one that has been abraded down to the base metal is only visible once you know what to look for.
If you run a gloved finger across the rotor after a few hundred miles, the texture alone can indicate whether the coating was applied too thick or too thin. A properly cured layer will exhibit a slightly tacky, almost waxy drag under light pressure, while a coating that has worn through feels cold and slick, with no resistance. Pay attention to the direction of the abrasion lines as well: radial scratches may come from debris caught in the pad, but circumferential grooves that follow the rotor's rotation are more likely caused by a coating that has begun to delaminate at the grain boundaries. Those grooves deepen over time, eventually creating a channel that compromises the pad's ability to form a consistent transfer film.
One field shortcut used by seasoned mechanics is to inspect the rotor under low-angle light after a hard stop. If the coating is still intact, you should see a faint, even bloom across the surface, like the haze on a freshly waxed car. Any dark, shiny patches that reflect light differently mean the coating has been worn away unevenly, and what you're seeing is the bare substrate beginning to gall. That's the moment to swap in a different pad compound or reassess the rotor's metallurgy—before the minor abrasion pattern turns into a full-blown failure that sends vibration up through the caliper.
When to Sacrifice Capacity for a Cleaner Seal
There are times when pushing a pump or mixer to its maximum rated capacity works against the very seal that keeps it running. High flow rates and pressures generate extra heat and shear at the sealing interface, which can deform elastomers or accelerate wear on hard faces. If you notice frequent leaks, discolored product near the seal, or rising maintenance costs, dropping the operating speed by ten to fifteen percent often brings the seal back into a stable temperature and pressure window. The loss in throughput is usually modest compared to the downtime avoided.
This trade-off becomes even clearer with sticky or abrasive media. In food and pharmaceutical lines, a product that contains sugar crystals, starches, or fine particulates can erode a seal face within days when the line runs at full blast. Running at a slightly lower capacity reduces the particle impact velocity and lets a film of process fluid lubricate the seal instead of scouring it. Some plants also choose a narrower clearance seal or a softer secondary lip, accepting a small drop in volumetric capacity in exchange for much longer runs between cleanings.
Sacrificing capacity for a cleaner seal is not a permanent downgrade; it is a deliberate operating choice. Test runs at reduced speed or pressure can show whether the seal stays cleaner and lasts longer. If the numbers work out, the higher uptime and lower contamination risk outweigh the lost nameplate capacity. Over time, you may even recover that capacity by resizing downstream equipment or adjusting batch schedules, without pushing the seal back into a failure-prone zone.
Rotor Tips That Don't Crack Under Thermal Shock
Thermal shock on rotor tips usually comes down to one thing: uneven expansion. When the outer edge heats faster than the center, it wants to grow, but the cooler metal holds it back. That tug-of-war creates micro-tears that eventually become visible cracks. A tip that survives this cycle isn't just about picking a harder alloy—it's about shaping the stress out of the part before it ever reaches the surface.
The practical fix starts with a low-expansion base material paired with a thin, high-conductivity skin. The skin spreads heat quickly so the temperature gradient across the tip stays shallow, while the core resists dimensional change. On top of that, adding a series of small radial relief grooves along the tip edge breaks up the continuous hoop stress that normally feeds crack growth. These grooves aren't decorative; they interrupt the stress path the same way scoring a glass cutter guides a break, but in reverse.
After repeated cycles from room temperature to over 700°F—far beyond what most brake or turbine rotors see in normal use—the tips show no crack initiation under dye penetrant inspection. That kind of margin means longer service life, fewer surprise teardowns, and a rotor that keeps its balance instead of turning into a vibration source.
Balancing Air Leakage Against Feed Accuracy
A rotary valve that seals perfectly against air leakage would seem ideal, yet in practice that same tight clearance can bind on fines or thermally expand until the rotor stalls. Feed accuracy suffers either way. When air escapes past the valve into a hopper or conveying line, it can fluidize powder at the pickup point, causing sudden density swings. The controller then chases a feed rate that never settles, because the weight signal reflects both material flow and pressure-driven noise.
Operators often respond by adjusting venting or adding a pressure-balancing line, but this only shifts the leak path rather than eliminating it. The more useful approach is to map where air is actually moving. Small leaks across a flexible connector rarely matter for coarse granules, yet the same gap can blow cocoa powder or fine cement out of suspension. Matching seal clearances to the material’s particle size and aeration tendency gives a better starting point than simply tightening everything.
On gravimetric feeders, a common workaround is to let the load cell see a stable baseline by isolating the feeder frame from line pressure fluctuations. Some setups introduce a controlled air purge upstream of the metering zone, accepting a small, constant leak because its effect can be calibrated out. The feed rate then remains repeatable even if the mass flow of air changes with line pressure. It is that repeatability, not the absolute absence of leakage, which keeps batch weights within tolerance.
Designing the End Plates for Real-World Maintenance
When end plates are buried behind layers of piping or tucked under a motor housing, maintenance stops being a routine task and turns into a small engineering project. A better approach is to treat the end plate as an access point from the start. That means leaving enough clearance for a torque wrench, choosing bolt patterns that don't force a technician to work blind, and avoiding recessed fasteners that fill with debris after a few months on the floor. If a plate needs to come off quarterly for seal inspections, it should never require removing three unrelated components first.
Material choice for the plate itself often gets decided by cost alone, but real-world maintenance tells a different story. In washdown areas, stainless steel plates with a light passivation layer resist pitting far longer than coated carbon steel, and they don't leave rust streaks on the equipment frame. For high-vibration machines, adding a small lip or thickening the flange around the bolt holes prevents the plate from working loose between scheduled checks. It's these practical details that reduce the number of unplanned shutdowns tied to leaking or cracked end plates.
Fastener selection is another place where design and maintenance drift apart. Using three different bolt sizes on one plate—common when engineers mix metric and inch hardware—guarantees a future headache. Standardizing on one size, one thread pitch, and one head type allows a single tool to handle the whole job. Including captive washers or using flanged bolts removes loose parts that get dropped into awkward corners. The goal isn't a perfectly elegant end plate on paper; it's one that a tired technician can remove, inspect, and reinstall in under ten minutes without swearing at the design team.
FAQ
A custom valve earns its keep when the material refuses to behave—high abrasion, sticky buildup, low melt temperatures, or aggressive pressure differentials. Standard castings rarely survive those conditions, so you start with the material's failure modes and design backwards.
You don't chase the tightest possible gap. For abrasive service, slightly larger clearances combined with hardfacing or replaceable tips often outlast a precision-machined rotor that galls or jams. The goal is a controlled leak path that stays stable rather than a zero-clearance fantasy.
Materials like cocoa powder or titanium dioxide can pack into deep V-shaped pockets and refuse to leave. Shallow, rounded, or asymmetrical pockets—sometimes with a blow-through or reduced-shear inlet—keep the fill and discharge cycle consistent and prevent stagnant zones.
Purged gland packing or air-purged shaft seals with a lantern ring work better than lip seals, which can melt or trap product. For high-temperature duties, a thermal isolation gap or water-cooled endplate keeps the seal zone below the material's softening point.
When the material is both abrasive and prone to leakage—like fine silica sand—fixed steel tips wear into a sloppy gap within weeks. Adjustable polymer or hardened tips let you restore effective sealing without pulling the valve, and flexible wipers help scrape the housing bore clean.
Venting arrangements and inlet geometry get less attention than motor size. Without a properly sized vent port on the return side, fines blow back into the inlet and kill feed accuracy. Likewise, ignoring the material's angle of repose when shaping the inlet can cause flooding or starvation.
Conclusion
Before cutting any metal for a custom rotary valve, spend real time on the bench with your material. Measure its angle of repose, moisture pickup, and how it compacts under pressure—these traits dictate pocket depth, clearance, and even rotor speed far more than a generic datasheet ever will. A valve that works flawlessly on free-flowing plastic pellets can bind or blow through on sticky filter cake. Next, look at where your current rotor wears: if abrasion lines run along the leading edge of the vanes, you need a hardfacing or tungsten carbide coating there, not just a thicker chrome plate. Sacrificing some pocket volume for a tighter tip-to-housing clearance often pays off in reduced air leakage and a cleaner seal, especially when feeding into a pneumatic line. And never ignore thermal shock—rotor tips that survive a 200°F process may crack when a cold purge cycle hits them; specify a ductile iron or fabricated steel tip with stress-relief details instead of a brittle cast alloy.
Balancing air leakage against feed accuracy is the quiet battle in every rotary valve. A little leakage can actually help fluidize some powders, but too much wrecks your metering consistency and wastes conveying air. Design the end plates with real maintenance in mind: bolt-on, replaceable wear strips and shaft seals that can be swapped without pulling the entire rotor. If the plates are welded into the housing, a simple seal replacement becomes a weekend shutdown. Instead, make the end plates sacrificial and field-adjustable, with oversized bearing carriers so you can shim the rotor back to center after wear. The best custom valves look unremarkable on the outside but are full of deliberate, hard-won details—clearances tuned to your material, coatings matched to your abrasion pattern, and end plates that a mechanic can service with basic tools, not a crane.
Contact Us
Contact Person: Ananda
Email: [email protected]
Tel/WhatsApp: 8619016718200
Website: https://www.wzaomi.com